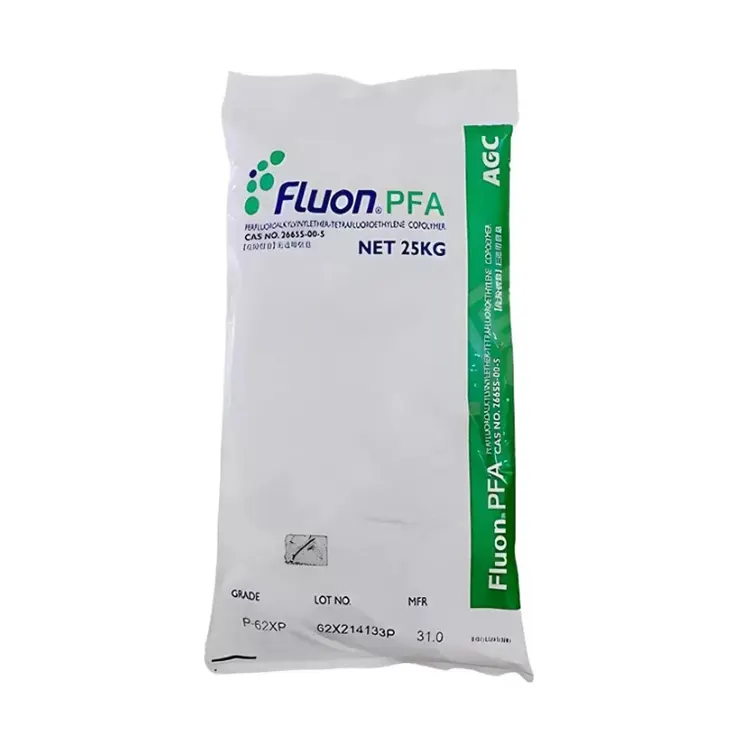
When purchasing High-MFR PFA for miniature molded components, Zhongwang helps industrial buyers compare melt flow characteristics with their actual mold geometry and processing requirements. The material is a melt-processable perfluoroalkoxy fluoropolymer with a relatively low molecular weight compared with medium- and low-MFR grades.
A higher melt flow rate makes it easier for molten resin to travel through narrow flow paths and fill thin sections before solidification. This characteristic is particularly useful for precision components containing small cavities, narrow channels, or complicated internal geometries.
Higher flowability, however, involves a material trade-off. Compared with lower-MFR grades, high-flow PFA generally has reduced melt strength and may offer less resistance to long-term creep or environmental stress cracking.
Consequently, this material is better suited to products requiring controlled filling and relatively thin sections than to thick-walled components exposed to substantial sustained pressure.
In micro-injection molding, resin must pass through gates, runners, and thin sections before the melt temperature decreases. Insufficient flow may cause short shots, incomplete corners, or inconsistent filling between cavities.
High-flow PFA can help address these challenges by reducing resistance to melt movement. The actual result depends on mold design, gate dimensions, melt temperature, injection pressure, and filling speed.
Wire insulation and micro-tubing require consistent material distribution around narrow cross-sections. Resin flow behavior influences extrusion pressure, coating uniformity, and dimensional consistency.
Suitable high-flow grades can be evaluated for fine-gauge insulation, small-diameter tubing, and other continuous extrusion applications where maintaining a thin polymer layer is important.
Compared with higher-viscosity PFA, a high-flow formulation may allow easier filling under otherwise comparable processing conditions.
This does not eliminate the need for appropriate equipment. Fluoropolymer-compatible screws, barrels, tooling materials, and temperature controls remain necessary.
High-MFR PFA is applicable to miniature valve inserts, small corrosion-resistant fittings, intricate instrument components, and non-pressure-bearing sample-cell housings.
For multi-cavity tooling, manufacturers should evaluate cavity balance, weld-line formation, flash, and dimensional variation during trial production.
High-speed extrusion grades can be considered for thin insulation layers on specialized wires and small coaxial cables.
The supplied reference identifies an MFR range of 16–30 g/10 min for this application category. Extrusion suitability also depends on die configuration, line speed, concentricity, and cooling conditions.
| Item | Reference Specification |
|---|---|
| Product Name | High-MFR PFA |
| Brand | Zhongwang |
| Material | Perfluoroalkoxy Fluoropolymer |
| Melt Flow Rate | 16–45 g/10 min (372°C/5 kg), grade-dependent |
| Density | 2.12–2.17 g/cm³ |
| Melting Point | 300–310°C |
| Tensile Strength | ≥24 MPa, typical reference |
| Elongation at Break | ≥250%, typical reference |
| Continuous Service Temperature | -200°C to 260°C, application-dependent |
| Dielectric Constant at 1 MHz | 2.15, typical reference |
| Flammability | UL94 V-0 at 1.5 mm, grade-specific reference |
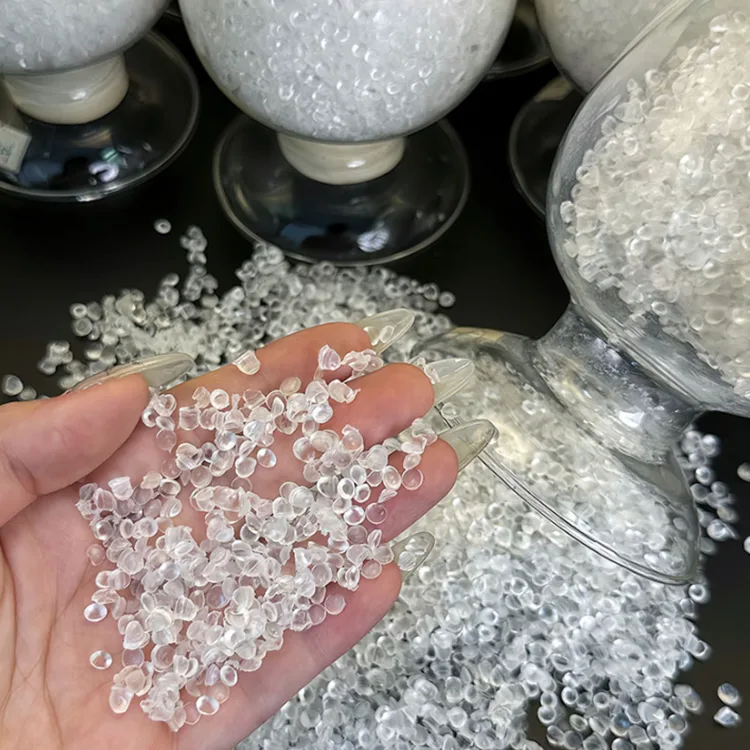
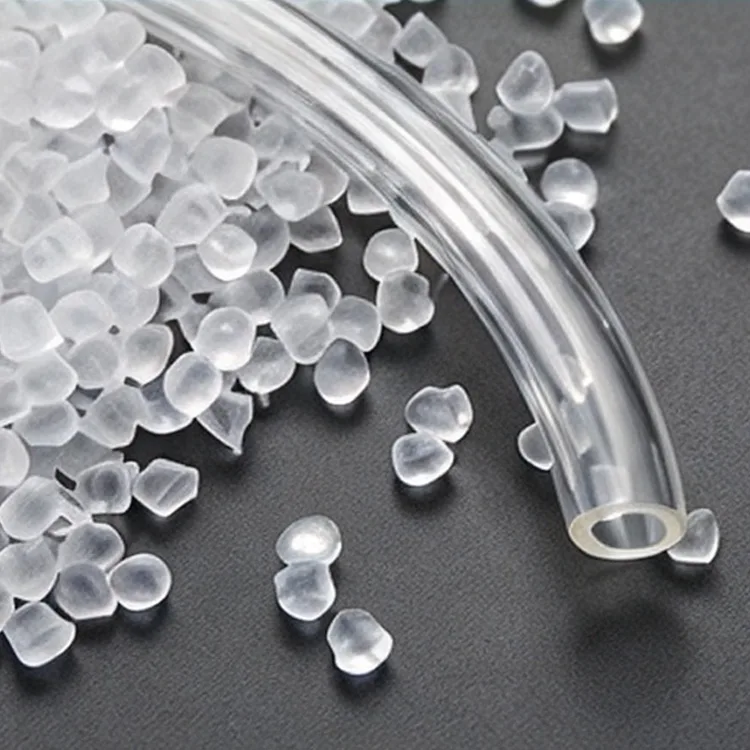
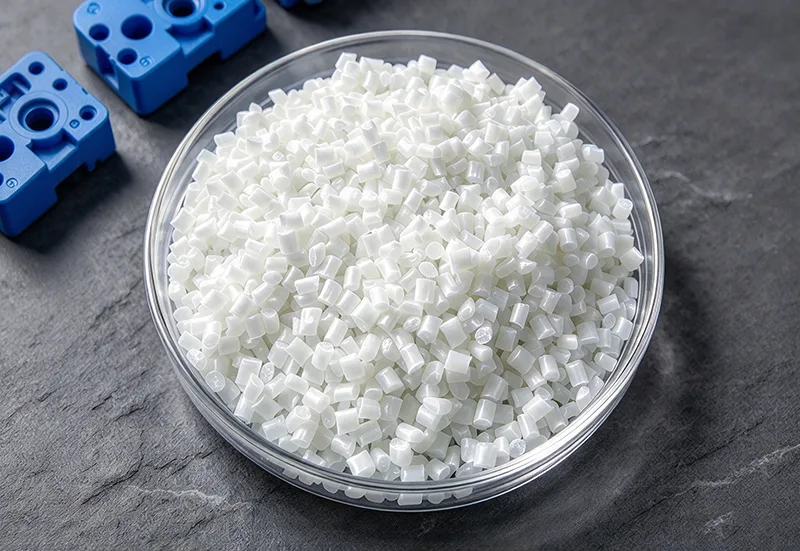
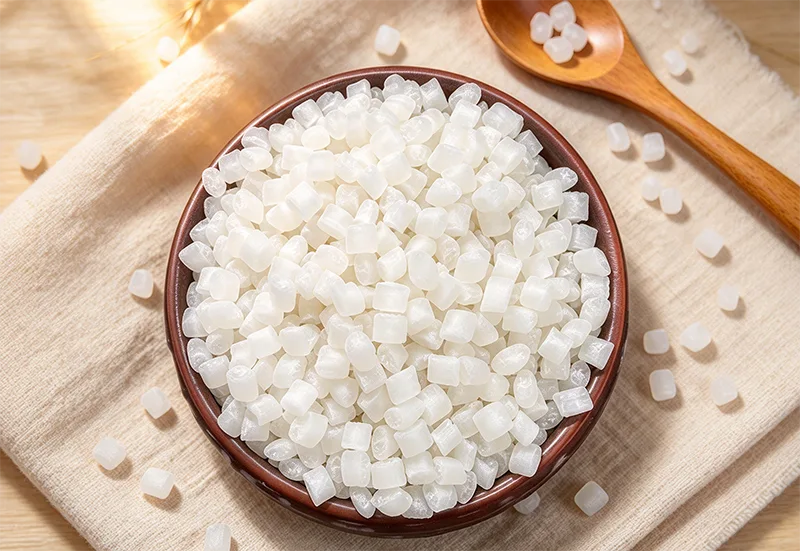
| Appearance | Translucent Ivory-White Pellets |
| Processing Methods | Injection Molding, Extrusion, Transfer Molding |
| Packaging | 25 kg PE Inner Bag and Paper Drum |
| Available Documents | TDS, COA, SDS and Applicable Test Reports |
The supplied technical reference identifies barrel temperatures of approximately 335–375°C and die temperatures of 355–390°C. These are processing references rather than fixed settings for every machine.
Extended exposure to excessive processing temperatures can degrade fluoropolymers and generate hazardous decomposition products. Equipment settings, residence time, ventilation, and shutdown procedures should follow the selected grade's processing and safety documentation.
Improved fluidity may increase the likelihood of flash when injection pressure, mold fit, or gate design is unsuitable. Weld-line strength should also be evaluated where multiple melt fronts meet.
Manufacturers should assess injection speed, pressure, cooling, and cavity geometry together instead of increasing material temperature as the only adjustment.
High-flow resin should not automatically be selected for thick-wall pressure fittings, tank linings, or diaphragms subject to significant long-term loading.
In these applications, a lower-MFR material may be more appropriate because melt strength, creep behavior, and stress-crack resistance become more important than rapid cavity filling.
Located in Yuyao China Plastics City, Zhejiang Zhongwang International Trade Co., Ltd. coordinates industrial resin procurement through established raw material sourcing and logistics channels.
For considering High-MFR PFA, the most useful quotation details are the target MFR, processing method, minimum wall thickness, cavity configuration, operating medium, and expected mechanical loading.
Where high-purity components are involved, metal-ion extractables and relevant technical documentation should be included in the purchasing requirements. Sample processing and finished-part testing are recommended before commercial approval.
Higher melt flow can help molten polymer fill narrow cavities and thin sections. Its suitability still depends on mold geometry, processing temperature, injection pressure, and the mechanical requirements of the finished part.
It can be evaluated for appropriate fittings, but high-flow grades are generally less suitable for components dominated by long-term creep or substantial pressure loading. Pressure requirements and stress-crack resistance should be checked before material selection.
Flash may result from excessive injection pressure, unsuitable temperature, mold clearance, or poor gate and cavity design. A higher-flow material requires careful adjustment of these processing conditions.
Applications involving sensitive process fluids may require specific limits for metal ions, extractables, and other impurities. The appropriate purity grade should be chosen against the actual fluid-contact requirements.
Address
Building 1, China Plastics International Business Center, No. 285 Shunda West Road, Yuyao City, Ningbo City, Zhejiang Province, China
Tel
If you have any enquiry about quotation or cooperation, please feel free to email us or use the following inquiry form.Our sales representative will contact you within 24 hours. Thank you for your interest in our products.